


Crude oil has limited direct usefulness until a refinery separates and prepares its many hydrocarbon components. Refining transforms crude feedstock into useful fuels, petrochemical feedstocks, lubricants, asphalt, and other valuable materials.
Refineries generally combine physical separation with chemical conversion. Physical operations separate naturally occurring components according to properties such as boiling point, while chemical processes deliberately alter molecules to improve yields, quality, and performance.
The physical refining stage normally begins after production, gathering, and preliminary handling of crude oil. **Crude oil composition** varies considerably between fields, so refinery operators must understand its characteristics before selecting suitable processing conditions.
Among the most important physical operations are desalting, dewatering, atmospheric distillation, and vacuum distillation. Together, these processes remove unwanted materials and separate crude oil into fractions that serve different industrial purposes.
This article explains how each major physical process works, why operators perform it, which products emerge from each stage, and how careful control improves refinery efficiency, equipment protection, and product quality.
Physical Refining Processes And Their Purpose
1. Feed Preparation: Refinery operators first inspect and prepare crude oil before major separation begins. This stage identifies water, salts, sediments, gases, and other contaminants that could interfere with downstream equipment.
2. Physical Separation: The refinery then separates crude components without deliberately changing their molecular structures. Distillation exploits differences in boiling points to produce streams with different volatility, density, composition, and intended uses.
3. Product Recovery: Physical separation creates several useful refinery streams, including gases, naphtha, kerosene, gas oils, vacuum gas oil, lubricating fractions, and residual materials for further processing or direct applications.
4. Equipment Protection: Removing water, salts, and sediments before distillation reduces corrosion, fouling, plugging, and catalyst problems in later refinery units. Proper preparation therefore supports safer operation and more reliable processing performance.
5. Yield Improvement: Accurate separation allows refiners to recover valuable fractions efficiently from the available feedstock. Better fractionation also gives operators greater control over product quality and the distribution of refinery outputs.
Crude oil contains hydrocarbons with widely different boiling characteristics, together with undesirable non-hydrocarbon materials. Understanding these components helps operators determine the correct temperatures, pressures, separation methods, and equipment arrangements for processing.
Information about crude oil composition helps explain why one crude stream can produce different quantities and qualities of refinery fractions compared with another source.
Physical refining also connects closely with the different petroleum fractions obtained after distillation, because each fraction possesses characteristic hydrocarbon structures and practical industrial applications.
Crude oil itself originates from geological processes, and its properties depend partly on the source material and geological environment. Understanding that background provides useful context for refinery feedstock selection and treatment requirements.
The wider origin of crude oil therefore matters because petroleum from different reservoirs can show substantial variations in wax, sulphur, metals, density, and boiling-range distribution.
These variations influence refinery design and operating decisions. A heavy, high-sulphur crude generally demands more careful preparation than a lighter feed containing fewer contaminants and producing a larger proportion of valuable light fractions.
Read Also : Mechanisms of Petroleum Migration and Petroleum Occurrence
Desalting And Dewatering Of Crude Oil
Desalting and dewatering provide the first major physical cleanup step for crude oil. Operators remove produced water, brine, dissolved salts, suspended solids, and other contaminants before atmospheric distillation begins.
Crude oil leaving a reservoir commonly carries formation water and mineral salts. Sediments may also enter production streams, while gases and other naturally associated materials can complicate transportation, storage, and refinery operations.
Operators commonly mix crude with carefully controlled wash water before sending it into an electrostatic desalter. The wash water dissolves salts, while electric fields help separate water droplets from the oil phase.
Inside the desalter, electric forces encourage small dispersed water droplets to combine into larger droplets. The heavier water settles downward, while treated crude remains above and moves forward toward the distillation train.
Removing salts protects refinery equipment because chloride compounds can contribute to corrosion, especially when they form acidic species under refinery operating conditions. Lower salt levels also reduce fouling and maintenance demands.
Effective dehydration also matters because excess water consumes heating capacity and can destabilize downstream operation. Reliable separation reduces unnecessary water circulation and helps maintain predictable feed conditions entering the furnace.
The importance of proper contaminant removal becomes clearer when examining industrial responsibility for waste management, because refinery activities must control both process efficiency and environmental impacts throughout production.
Crude oil contaminants can also influence corrosion and environmental risks. Broader discussions of oil pollution sources and environmental effects show why careful handling remains important before, during, and after refinery processing.
Atmospheric Distillation Of Crude Oil

1. Feed Heating: Desalted crude enters a furnace, where operators heat it to a temperature that vaporizes much of the feed without intentionally encouraging significant thermal cracking of the hydrocarbons.
2. Tower Entry: The heated mixture enters an atmospheric fractionation tower containing internal trays or packing. Rising vapours contact descending liquid streams repeatedly, allowing components to separate according to their boiling characteristics.
3. Fractionation: Lighter hydrocarbons travel higher within the tower because they vaporize more readily, while heavier materials remain lower. Temperature gradually decreases toward the top and increases toward the bottom.
4. Product Withdrawal: Refiners withdraw several side streams and overhead products from selected tower locations. These streams typically include gases, naphtha, kerosene-range materials, gas oils, and heavier atmospheric residue.
5. Reflux Control: Condensed overhead liquid returns to the tower as reflux. This reflux improves contact between vapour and liquid phases, sharpening separation and helping operators maintain desired boiling-range specifications.
Atmospheric distillation does not normally create new hydrocarbon molecules. Instead, it separates existing components according to their volatility, which makes the process one of the central physical refining operations in every conventional refinery.
Knowledge of the petroleum transformation process helps place atmospheric distillation within the wider petroleum lifecycle, from geological formation through extraction, separation, transportation, refining, and final product use.
Atmospheric distillation commonly produces light and middle fractions that require additional treatment before they meet commercial specifications. Nevertheless, the initial separation establishes the feed streams needed for later refinery units.
The atmospheric tower therefore acts as a major distribution point, directing materials toward gasoline, kerosene, diesel, lubricant, fuel-oil, and conversion processes according to refinery design and market requirements.
Figure: Flow sheet of Atmospheric Distillation Process Crude Oil (Speight 2006)
Major Fractions From Atmospheric Distillation

1. Refinery Gases: The lightest materials leave near the top of the atmospheric tower. They include methane, ethane, propane, butane, and other light components that refineries can recover, blend, or process.
2. Naphtha: Naphtha occupies a relatively light boiling range and commonly serves as gasoline feedstock or petrochemical feedstock. Its final value depends strongly on composition and subsequent upgrading requirements.
3. Kerosene: Kerosene-range material forms an important middle distillate stream. Refineries may direct suitable portions toward household fuels, aviation fuel manufacture, or other processes after additional quality treatment.
4. Gas Oils: Gas oils boil at higher temperatures than kerosene and can supply diesel-related processing streams, heating products, or feedstock for catalytic conversion units that increase yields of valuable lighter products.
5. Atmospheric Residue: The heaviest material remains near the tower bottom because its components require higher temperatures to vaporize. Refineries normally send this residue to a vacuum distillation unit.
The exact quantity and quality of each fraction depend on crude characteristics and operating conditions. A refinery processing lighter crude may obtain more valuable light products than one processing heavier crude.
Detailed information about petroleum fraction components shows how paraffins, naphthenes, aromatics, and other compounds distribute across the boiling ranges obtained during physical separation.
Crude composition also affects fraction quality because hydrocarbons and non-hydrocarbon compounds do not distribute uniformly throughout the distillation range. Heavier fractions usually contain more complex molecules and undesirable contaminants.
For this reason, the fractionation tower provides separation rather than final product purification. Many withdrawn streams still require additional treatment, blending, or chemical conversion before they become saleable petroleum products.
The relationship between crude composition and refinery output also explains why refineries evaluate feedstock properties carefully. Operators can then adjust temperatures, reflux rates, pressures, and product draw rates for better performance.
Vacuum Distillation For Heavy Crude Fractions
1. Residue Feed: Vacuum distillation receives the heavy atmospheric residue that remains after the first distillation stage. This material contains valuable high-boiling components that atmospheric equipment cannot separate safely.
2. Reduced Pressure: The vacuum tower lowers system pressure, allowing heavy hydrocarbons to vaporize at lower temperatures than they would require under normal atmospheric conditions.
3. Gentle Separation: Lower operating pressure reduces the need for excessively high temperatures. This approach helps limit undesirable thermal cracking while enabling recovery of useful heavy distillate streams.
4. Product Recovery: The vacuum tower separates materials such as vacuum gas oil and lubricant-range fractions from heavier residue. Refiners can send these streams toward additional processing or specialised product manufacture.
5. Residue Handling: Material that remains after vacuum separation becomes vacuum residue. Depending on refinery design and market demand, operators can use it for asphalt, fuel production, or further conversion.
Vacuum distillation developed because heavy petroleum components can crack when refiners expose them to sufficiently high atmospheric boiling temperatures. Reduced pressure changes the boiling relationship and enables safer separation.
The process therefore extends physical separation beyond the practical limits of atmospheric distillation. It extracts additional useful material from heavy crude residue without relying on deliberate molecular conversion.
Heavy crude streams commonly contain greater quantities of complex compounds and metals. Information on the nature of petroleum occurrence helps explain why crude characteristics vary between producing regions and reservoirs.
Vacuum operation also requires careful pressure control because unstable vacuum conditions can disturb vapour flow, separation efficiency, and product quality. Well-designed systems therefore manage pressure, temperature, residence time, and feed distribution closely.
Heavy refinery streams require responsible management because their properties influence subsequent conversion, handling, storage, and environmental controls. Refinery design must therefore balance recovery, safety, product quality, and operational reliability.
Vacuum Products And Heavy Residue Uses
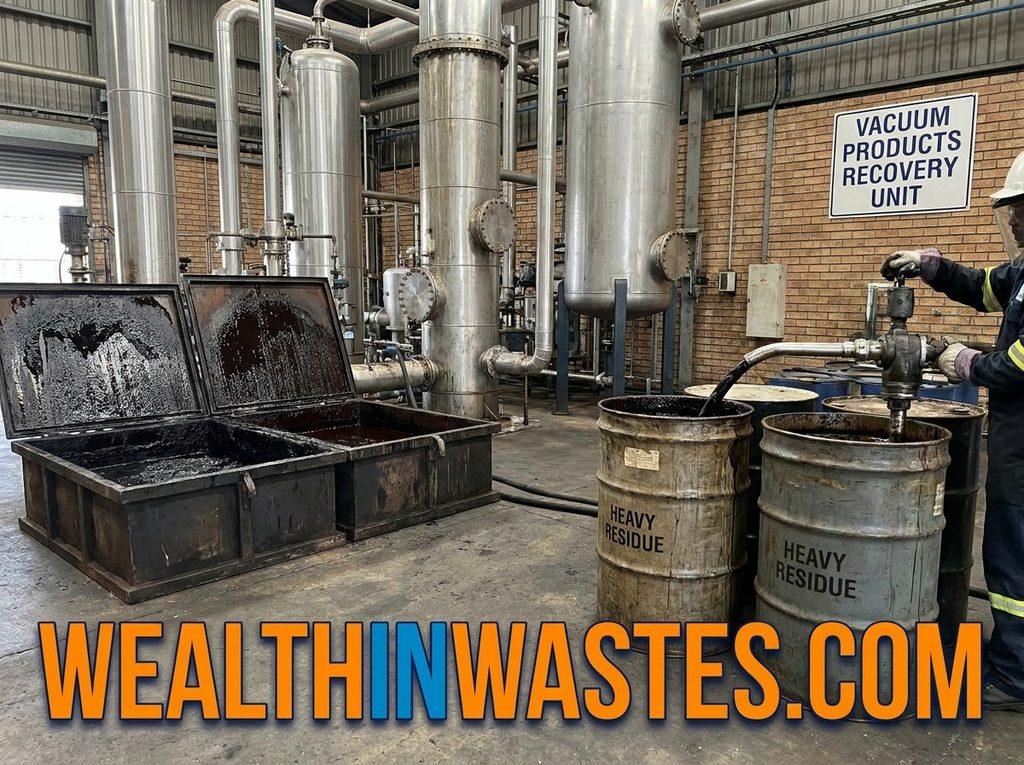
Vacuum distillation produces several heavy streams that remain economically important. Their uses depend on composition, viscosity, boiling range, contaminant content, refinery configuration, and the availability of downstream processing units.
Vacuum gas oil can serve as feedstock for conversion units, especially where refineries need to transform heavier molecules into lighter, more valuable transportation-fuel components.
Lubricating fractions can undergo additional processing to produce base oils or other specialised materials. Their quality depends on molecular composition, contaminants, viscosity characteristics, and subsequent refining requirements.
Vacuum residue forms the heaviest stream and contains highly complex molecules, including substantial concentrations of compounds containing sulphur, nitrogen, metals, and other heavy constituents.
Some refineries use heavy residue for asphalt production, while others send it toward thermal or catalytic conversion processes. The selected route depends on equipment availability, crude characteristics, product demand, and economics.
The behaviour of heavy petroleum streams also relates to broader discussions of oil contamination and environmental fate, because spills involving persistent heavy materials can create significant cleanup and ecological challenges.
Refinery operators therefore treat heavy fractions as valuable feedstocks rather than useless leftovers. Correct separation can increase recovery and create more options for subsequent processing, blending, storage, transportation, and commercial use.
Understanding heavy fractions also helps explain why crude oil refineries rarely rely on atmospheric distillation alone. Vacuum separation unlocks additional value from the material remaining after the initial fractionation stage.
Heavy fractions may contain components that challenge downstream equipment, especially when metals, sediments, sulphur compounds, or other contaminants remain significant. Effective feed preparation therefore supports stable operation across the entire refinery.
The physical refining sequence ultimately determines where each portion of the crude stream goes. Refiners can then select chemical conversion or finishing processes according to the properties and commercial objectives of each separated fraction.
Process Control And Crude Oil Quality
Effective physical refining depends on precise control of temperature, pressure, flow rate, reflux, feed quality, and separation efficiency. Small operating changes can influence fraction yields, energy consumption, equipment stability, and product quality.
Operators continuously monitor crude feed characteristics because different crude oils require different operating strategies. Density, viscosity, water content, salt level, sulphur level, and boiling behaviour can significantly affect unit performance.
Laboratory analysis supports these operating decisions by identifying important feed properties before and during processing. Better information helps operators maintain stable separation conditions and detect unusual changes in incoming crude streams.
Equipment reliability also depends on controlling contaminants. Discussions of industrial wastewater treatment demonstrate why refineries must manage process water and contaminated effluents carefully alongside their primary production activities.
Refinery waste streams can include oily water, sludge, contaminated solids, and other materials requiring appropriate treatment. These concerns connect physical refining with wider industrial waste management practices.
Hazard management also becomes important when workers handle crude oil, hot hydrocarbons, contaminated water, and refinery residues. Understanding hazardous waste sources supports safer planning for storage, transport, treatment, and disposal.
Strong process control improves energy efficiency because operators can avoid unnecessary overheating and unstable circulation. Consistent conditions also help maintain the desired cut points between neighbouring distillation fractions.
Quality control therefore extends beyond producing the correct fraction. It also involves maintaining predictable composition, minimizing contamination, preserving equipment integrity, and directing each separated stream toward its most suitable downstream destination.
Refinery personnel must also understand the environmental consequences of uncontrolled releases. The wider effects of water pollution explain why petroleum-related releases require prompt prevention, containment, treatment, and monitoring.
Read Also: Roles of Producers and Corporations in Waste Management
Environmental And Operational Considerations
Although physical refining does not intentionally change hydrocarbon molecules, it still creates environmental and operational challenges. Refineries consume energy, handle hazardous materials, generate wastewater, and manage emissions and contaminated residues.
Water used during desalting eventually becomes part of a contaminated wastewater stream containing salts, suspended solids, oil, and other substances. Proper treatment helps protect receiving environments and supports regulatory compliance.
Air emissions can arise from furnaces, storage systems, flaring, leaks, and other refinery activities. Broader information on air pollution and its impacts highlights why emission control remains important around industrial facilities.
Oil-containing materials can also create hazardous waste concerns when poorly managed. The principles described in hazardous waste control emphasize proper identification, handling, storage, treatment, and disposal practices.
Pollution prevention should begin during process design rather than after contamination occurs. The broader concept of pollution abatement and control supports this preventive approach across refinery operations.
Refineries can also reduce environmental risks through leak detection, secondary containment, wastewater treatment, equipment maintenance, process optimization, and responsible management of recovered materials and generated residues.
Environmental performance matters economically as well as ecologically because pollution incidents can create cleanup expenses, production losses, legal liabilities, damaged infrastructure, and community disruption. Studies of economic losses from pollution illustrate these wider consequences.
Refinery operators should therefore view physical refining as part of an integrated production system. Efficient separation must work alongside pollution prevention, waste treatment, worker safety, energy management, and responsible resource use.
The environmental dimension becomes especially important in petroleum-producing regions, where extraction, transportation, refining, and waste handling can affect land and water resources. Strong controls help reduce avoidable damage across the petroleum value chain.
Broader discussions of sources and types of water pollution also show why petroleum-related wastewater and accidental releases deserve careful attention during refinery planning and environmental monitoring.
Environmental management should continue after physical separation ends. Effective facilities monitor waste streams, maintain treatment systems, inspect equipment regularly, and respond quickly whenever abnormal releases or operating conditions occur.
Summary on Physical Refining Processes of Crude Oil
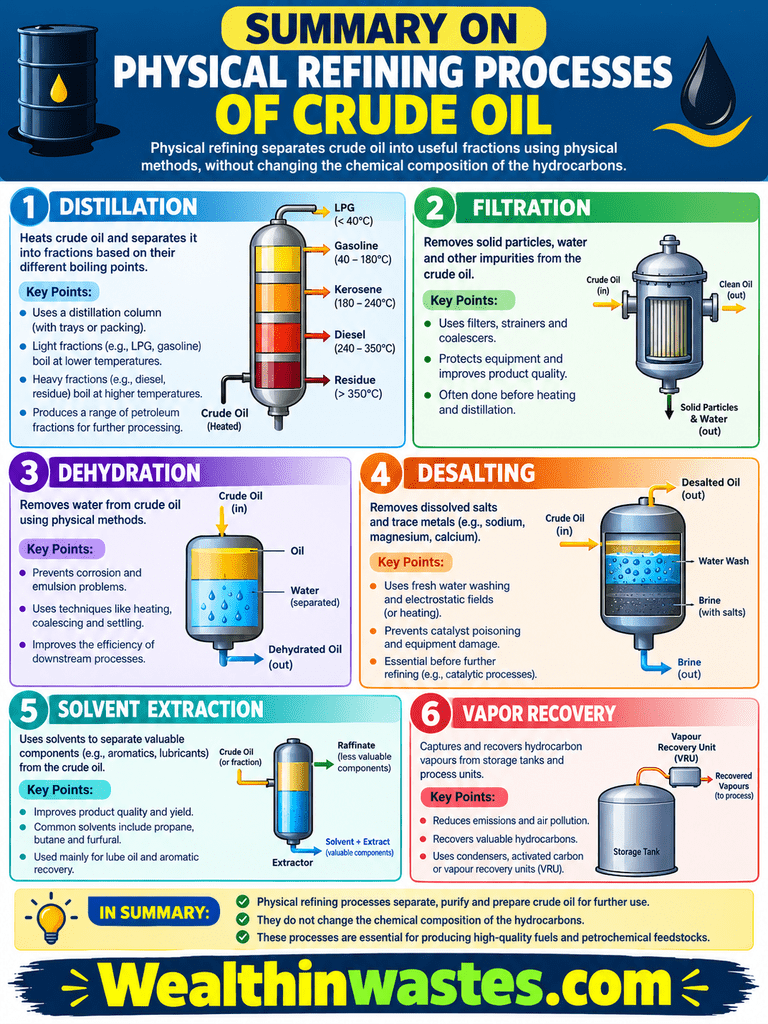
| Process | Main Purpose | Major Outcome |
|---|---|---|
| Desalting and Dewatering | Remove water, salts, and solids | Cleaner crude feed |
| Atmospheric Distillation | Separate crude by boiling range | Gases, naphtha, kerosene, gas oils, residue |
| Vacuum Distillation | Separate heavy residue at lower pressure | Vacuum gas oil, lubricant fractions, vacuum residue |
| Process Control | Maintain stable temperature, pressure, flow, and reflux | Consistent yields and quality |
| Environmental Management | Control wastewater, emissions, residues, and releases | Safer and more sustainable refinery operation |
Frequently Asked Questions About Physical Refining Processes of Crude Oil Explained
1. What are the main physical refining processes?
The main processes are desalting, dewatering, atmospheric distillation, and vacuum distillation.
2. Does physical refining change crude oil chemically?
Normally, physical refining separates existing components without deliberately changing their molecular structures.
3. Why does crude oil need desalting?
Desalting removes salts and water that can cause corrosion, fouling, plugging, and operating problems.
4. What does atmospheric distillation produce?
It separates crude into gases, naphtha, kerosene, gas oils, and atmospheric residue.
5. Why do refineries use vacuum distillation?
Vacuum distillation separates heavy hydrocarbons at lower temperatures and helps reduce thermal cracking.
6. What is vacuum residue used for?
Vacuum residue may serve as asphalt feedstock, fuel material, or feedstock for additional conversion processes.
7. Why does crude composition matter?
Crude composition determines fraction yields, contaminant levels, operating requirements, and the suitability of different refining routes.
8. How does physical refining support the environment?
Good physical refining improves efficiency and supports better control of wastewater, contaminants, emissions, residues, and accidental releases.
Do you have any questions, suggestions, or contributions? If so, please feel free to use the comment box below to share your thoughts. We also encourage you to kindly share this information with others who might benefit from it. Since we can’t reach everyone at once, we truly appreciate your help in spreading the word. Thank you very much for your support and for sharing!
Read Also: How to Start a Small-Scale Agro-processing Business